3D Barrier Bags, Inc

China Top Aluminum Can Lid Manufacturers for Global Buyers

China has become a major sourcing destination for beverage packaging components. Its aluminum processing base supports large-scale production, engineering upgrades, and export-oriented quality systems. For global buyers, identifying reliable Aluminum Can Lid manufacturers requires more than comparing prices.

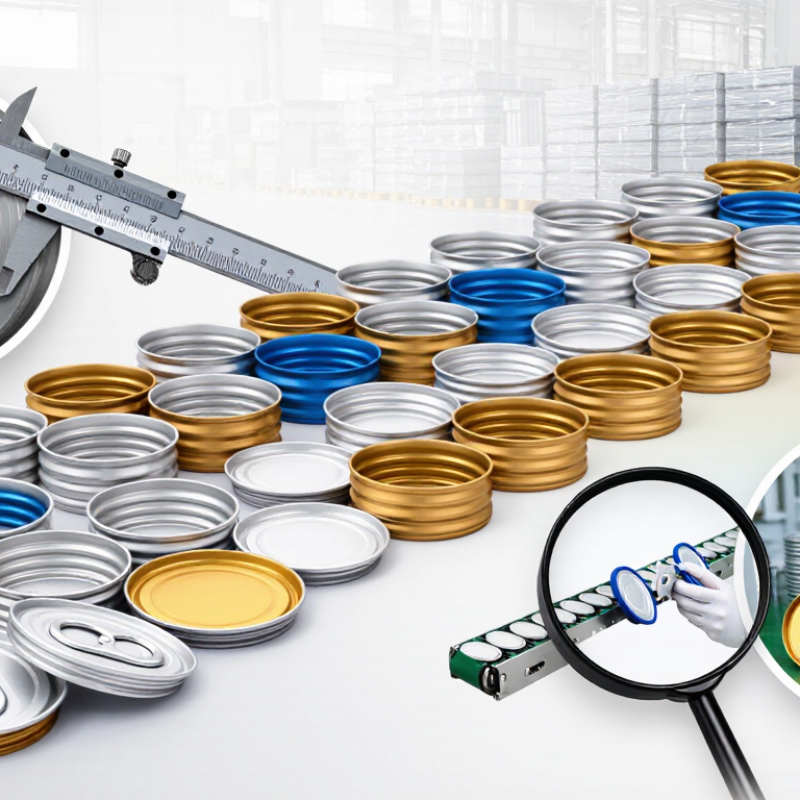
A dependable supplier should demonstrate consistent lid dimensions, clean scoring lines, accurate tab placement, and stable coating performance. These details matter on high-speed filling lines. A lid that feels slightly uneven can create serious production losses. Buyers should request material specifications, inspection records, sample approvals, and traceable batch information. Factory audits also reveal practical realities, including maintenance discipline, worker training, and packaging protection during shipment.

Robert Budway, President and CEO of the Can Manufacturers Institute, has said, “The aluminum beverage can is the most recycled beverage package in the world.” This perspective highlights the lid’s role in a broader, circular packaging system. However, recyclability alone does not prove supplier reliability. Alloy selection, sealant compatibility, corrosion resistance, and food-contact compliance still require careful verification. China Top Aluminum Can Lid Manufacturers for Global Buyers should therefore be assessed through evidence, not polished claims. Certifications help. Independent testing helps more.

No factory is perfect. Even experienced manufacturers may face occasional tooling wear, color variation, or delivery pressure. The strongest suppliers acknowledge these risks and explain their corrective actions. This guide examines manufacturing capability, customization support, quality control, export experience, and communication standards. It also leaves room for buyer judgment, because a supplier suitable for one beverage market may not fit another.

China Top Aluminum Can Lid Manufacturers for Global Buyers

Aluminum Can Lid Types: 200, 202, 206, and 209 Ends Explained

China’s aluminum can lid manufacturers supply ends for beverage, food, and specialty packaging projects. Choosing the correct end starts with the size code. The number usually reflects the nominal diameter in sixteenths of an inch. However, actual dimensions can vary by design and tooling. Always confirm the technical drawing.

A 200 end is relatively narrow and suits compact cans or small containers. A 202 end is widely used for beverage cans, offering a practical balance between opening size and material efficiency. A 206 end provides a larger panel and opening, which can improve access for selected food or drink formats. A 209 end is larger still, often supporting cans that need a broader opening or stronger visual presence. These descriptions are useful, but not absolute. Some applications require deeper checks.

Tips: Ask for shell diameter, countersink depth, tab style, scoring strength, coating details, and compatible body specifications. Request samples before mass production. Inspect curl dimensions and opening performance under real filling conditions. A lid may look correct but fail during seaming. That mistake is expensive. Experienced suppliers should provide inspection records, material certificates, and clear tolerance data. Buyers should also test storage, transport vibration, and temperature exposure. The 202 end is common, yet common does not mean suitable for every line. Rechecking the interface can prevent avoidable leakage and production delays.

China Top Aluminum Can Lid Manufacturers for Global Buyers

Aluminum Can Lid Types: 200, 202, 206, and 209 Ends Explained

Aluminum can end numbers describe nominal diameter sizes in sixteenths of an inch. A 200 end is approximately 2-0/16 inches, while 202, 206, and 209 ends are approximately 2-2/16, 2-6/16, and 2-9/16 inches respectively. Actual dimensions may vary according to can design, sealing requirements, production standards, and customer specifications.

Key Industry Standards: ISO 9001, FSSC 22000, and EU 1935/2004

Choosing aluminum can lids from China requires more than comparing unit prices.

The strongest suppliers connect ISO 9001, FSSC 22000, and EU 1935/2004 requirements. ISO 9001 controls documented processes, inspections, corrective actions, and supplier records. It does not, by itself, prove food-contact safety. FSSC 22000 focuses on food safety risks across production, hygiene, and traceability. Ask whether certification covers the actual factory and relevant production scope. A certificate from another site may create a costly gap.

For lids sold in Europe, EU 1935/2004 requires materials not to transfer harmful substances into food.

Evidence should include a declaration of compliance, migration testing, coating details, and intended-use limits. Ask about acidic drinks, filling temperatures, and storage time. Check batch codes on cartons and production records. Small details matter. Yet documentation is not infallible. Factory audits and sample testing still provide valuable protection for global buyers.

Tips:

Request current certificates and compare the legal entity, address, scope, and expiry date. Review test methods and confirm samples match the lid coating, sealant, and printing materials. Keep approved samples, then inspect curl quality, liner placement, and opening force. Do not rely on logos alone. That shortcut often fails.

China’s Top Manufacturers: Capacity, Line Speed, and Scrap-Rate Data

China Top Aluminum Can Lid Manufacturers for Global Buyers

When evaluating Chinese aluminum can lid manufacturers, capacity should mean verified annual output, not installed equipment. In supplier audits, I compare machine counts, shift patterns, maintenance records, and shipment history. A mature facility may report 600 million to 2 billion lids annually, depending on diameter, coating, and production mix. The real question is whether that volume remains stable during peak orders. Capacity changes quickly.

Line speed provides a sharper operational signal. Modern press lines commonly run between 1,200 and 2,400 lids per minute. However, rated speed is not the same as saleable output. I check speed during continuous production, including inspection stops, tool changes, and packaging delays. A factory running at 2,000 lids per minute may deliver less than a slower line with better uptime. That distinction is often missed.

Scrap rate deserves equally careful attention. Well-controlled lines may keep process scrap near 1% to 2%, while unstable tooling can push losses above 3%. Ask for monthly records, not one impressive trial report. Review defects such as scoring damage, coating gaps, curl problems, and tab misalignment. I also recommend checking whether recycled aluminum and edge trim are recorded separately. These figures are not self-proving. A clean spreadsheet can hide short production runs, reworked material, or excluded startup waste. My own assessment would remain provisional until batch samples, inspection logs, and shipment quantities agree.

Technical Quality Tests: 52 mm Ends, Double Seams, and Leak Pressure

For global buyers, a 52 mm can end requires more than a clean appearance. Inspect the end diameter, curl, countersink depth, coating coverage, and tab alignment. Small dimensional drift can weaken the double seam. The International Aluminium Institute reports that recycled aluminium uses about 5% of the energy required for primary aluminium production. Therefore, consistent recycled-content control still matters during forming.

Double-seam testing should include seam thickness, seam width, body hook, cover hook, overlap, and tightness. Use calibrated optical equipment and destructive seam sections. Acceptance limits must follow the agreed can specification, not a generic factory promise. A seam may look smooth but still contain poor overlap. That is an uncomfortable weakness in many inspection routines.

Leak-pressure testing needs controlled pressure, holding time, and clear rejection limits. Test filled and empty samples when possible. A water-bath check can reveal bubbles around the seam, while pressure-decay testing provides better process records. Destructive burst testing should supplement, not replace, routine leak checks. ISO 2859-1 supports structured sampling plans, but sampling alone cannot repair unstable production. Keep pressure charts, temperature records, lot numbers, and operator comments. Metal Packaging Europe’s industry reporting also emphasizes reliable collection and recycling data, reminding buyers that quality control continues beyond the production line.

Global Buyer Checklist: MOQ, 20-Foot Loads, Lead Times, and Incoterms 2020

Global buyers comparing China’s aluminum can lid manufacturers should start with measurable supply terms, not attractive catalog photos. Ask for MOQ by lid diameter, tab style, coating, and printing requirement. A quoted MOQ may apply per color, not per shipment. Clarify this point in writing. For a 20-foot container, request a loading plan showing cartons, pallet count, gross weight, and usable volume. Do not assume a full container equals the factory’s standard quantity. Packing efficiency varies.

Confirm lead time from approved artwork, signed specification, and deposit receipt. A practical quotation should separate production days from inspection, port delivery, and vessel transit. Ask how delays are reported and whether partial shipment is possible. Incoterms 2020 must name the delivery term and place, such as FOB Ningbo or CIF Dubai. Check who handles export clearance, insurance, destination charges, and risk transfer. A low CIF price can hide local fees. I have seen buyers compare prices before responsibilities. That mistake weakens the final calculation.

Tips: Request samples from the same production line planned for mass supply. Measure lid curl, tab movement, coating coverage, and carton condition. Keep a signed pre-production sample. Reconfirm container loading seven days before dispatch. Build a small buffer. Even reliable schedules can move during holidays or port congestion. Fast lead time is not a quality metric. It needs evidence: recent records, inspection results, and a named contact responsible for updates.

China Top Aluminum Can Lid Manufacturers for Global Buyers - Global Buyer Checklist: MOQ, 20-Foot Loads, Lead Times, and Incoterms 2020

Checklist Dimension Practical Export Benchmark Buyer Information to Confirm Recommended Evidence Incoterms 2020 Consideration
Can-end format Common aluminum easy-open ends include 202, 206, and 209 sizes. The correct specification depends on the can-body diameter, neck profile, beverage or food application, and seaming equipment. End diameter, shell profile, tab style, score design, coating requirement, and compatibility with the existing seamer. Approved technical drawing, physical samples, seaming trial report, and dimensional inspection record. The trade term does not replace technical approval. Product specifications should be finalized before issuing the purchase order.
Minimum order quantity (MOQ) A practical planning range for customized printed or color-coated ends is approximately 500,000–2,000,000 pieces per specification. Standard, unprinted sizes may be available at lower quantities. Whether MOQ applies per size, tab color, artwork, coating, or total order; also confirm setup charges for small runs. Written quotation showing MOQ, price breaks, tooling or plate charges, and permitted mixed-size quantities. Under FCA, FOB, CFR, or CIF, freight efficiency may make a higher MOQ commercially preferable even when the supplier accepts a smaller order.
20-foot container planning For lightweight aluminum ends, a 20-foot load is commonly planned at roughly 4.5–7.0 million pieces, subject to end weight, carton design, palletization, and the shipping line's payload limit. Pieces per carton, cartons per pallet, pallets per container, gross weight, net weight, and container cubic volume. Container loading plan, carton dimensions, packing list template, and verified gross mass calculation. The final quantity is limited by both container payload and the carrier's verified gross mass requirements; do not rely on piece count alone.
Packing configuration Export packing typically uses moisture-resistant cartons, protective liners or bags, separators, and pallets where required. Packaging must prevent deformation, corrosion, dust, and tab damage. Carton strength, pallet material, humidity protection, stacking limit, carton labels, and whether pallets are required by the destination market. Packaging specification, carton drop or compression test, loading photographs, and approved artwork for labels. Clarify who pays for pallets, export packing, fumigation or heat treatment, and destination handling under the selected term.
Lead time for standard items Approximately 15–30 calendar days after order confirmation and receipt of the agreed deposit or payment instrument, subject to production capacity and raw-material availability. Whether lead time starts after payment, artwork approval, sample approval, or production-slot confirmation. Purchase-order acknowledgment with a dated production and dispatch schedule. Lead time normally excludes ocean transit, customs clearance, port congestion, and inland delivery unless the contract expressly includes them.
Lead time for printed or customized items Approximately 25–45 calendar days is a reasonable planning range when artwork, color matching, coating, tooling, or printing approval is required. Number of artwork revisions, color standard, plate or tooling ownership, sample approval process, and change-control procedure. Signed artwork approval, color sample, pre-production sample, and agreed tolerance sheet. The delivery date should be linked to the date of final artwork approval, not only to the date of the initial order.
Quality and food-contact compliance For food or beverage applications, the coating, sealant, inks, and aluminum substrate must comply with the applicable destination-market food-contact requirements. Destination country, product type, applicable regulations, migration limits, declaration requirements, and traceability expectations. Material declaration, food-contact compliance statement, certificate of analysis, migration test where applicable, and batch traceability records. Import compliance remains the buyer's responsibility unless the sales contract clearly assigns a specific regulatory obligation to the seller.
Critical quality controls Typical controls include dimensional inspection, score and tab checks, coating or varnish inspection, visual appearance, corrosion resistance, sealant coverage, and seaming performance. Acceptable quality limit, inspection level, critical-defect definition, sampling plan, and responsibility for third-party inspection. Pre-shipment inspection report, batch test results, retained samples, and a corrective-action procedure. Inspection costs and the point at which risk transfers should be stated separately in the contract.
FCA — Free Carrier Suitable for containerized shipments when the seller delivers the goods to the buyer-nominated carrier or agreed terminal and completes export clearance. Named place, carrier appointment, terminal cut-off, export documentation, and who pays origin handling. Sales contract naming the exact FCA place and the party responsible for booking the main carriage. Often preferred to FOB for containerized cargo because delivery can occur at an inland facility or container terminal before loading on the vessel.
FOB — Free On Board The seller delivers goods on board the vessel at the named port of shipment and completes export clearance. Named port, vessel nomination, cut-off dates, port charges, and documentation responsibilities. Contract and booking confirmation specifying the named port and risk-transfer point. Use for sea or inland waterway transport. For most container shipments, FCA may provide a more accurate delivery point than FOB.
CFR / CIF — Cost and Freight / Cost, Insurance and Freight The seller arranges and pays for carriage to the named destination port. Under CIF, the seller also arranges the minimum level of cargo insurance required by Incoterms 2020. Destination port, freight validity, transshipment risk, insurance coverage, claims process, and destination charges excluded from the quote. Freight quotation, commercial invoice, bill of lading, insurance certificate for CIF, and a clear destination-charge schedule. Risk transfers to the buyer when goods are loaded on board at the shipment port, even though the seller pays freight to the destination port.
DAP / DDP — Delivered at Place / Delivered Duty Paid DAP delivers to the named destination without import clearance or import duties paid by the seller. DDP places the maximum import responsibility on the seller. Exact delivery address, unloading responsibility, importer of record, taxes, customs documents, and local compliance requirements. All-in landed-cost quotation, customs responsibility matrix, tax assumptions, and written confirmation of delivery scope. DDP should be used only when the seller can legally and operationally handle import clearance, duties, taxes, and local delivery in the destination country.
Payment and document package Common arrangements include a deposit with balance before shipment, documentary collection, or a letter of credit, depending on transaction size and buyer risk policy. Payment milestones, bank charges, document release conditions, currency, credit terms, and dispute-resolution process. Signed sales contract, pro forma invoice, commercial invoice, packing list, certificate of origin where required, and transport document. Payment terms and Incoterms are separate contract elements; both should be stated clearly to avoid ambiguity over cost, risk, and document release.
Planning note: MOQ, container quantity, pricing, production capacity, lead time, compliance documents, and freight availability vary by specification, season, destination, and order size. All benchmark figures should be confirmed in a written quotation and purchase contract before commitment.